Two Zero-Defect Regimes: Regulated Pharma & 24/7 Extrusion
Pharmaceutical packaging and industrial cable/pipe extrusion sit at opposite ends of the factory spectrum yet share one non-negotiable rule: a single unreadable code scraps product. In pharma, DSCSA / EU FMD / GMP serialization rejects any carton whose 2D ECC200 DataMatrix grades below ISO 15415 threshold; on a PVC wire or HDPE water-pipe extruder, losing meter-mark continuity during a 72-hour run forces scrapping hundreds of meters of pipe. Grounded in packaging coding applications and inkjet coding inks and specs, we engineer dedicated solutions for both.
Pharma cartoners pair 600 × 600 dpi OEM TIJ + inline vision cameras; extrusion lines pair agitated white/yellow pigmented CIJ + dual-wheel precision encoders.
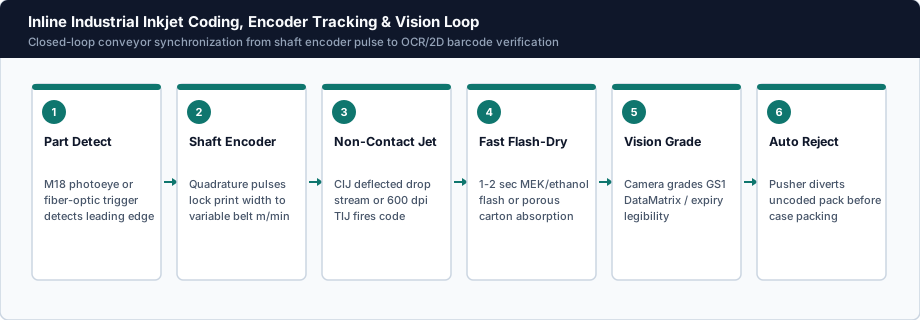
Pharma Track-and-Trace vs Extrusion Meter-Marking Specs
Side-by-side comparison of hardware, software, and ink requirements:
| System Element | Pharma Carton / Blister Serialization | Wire, Cable, Hose & Pipe Extrusion |
|---|---|---|
| Core Printer Platform | 600 × 600 dpi OEM TIJ (Wolke m610 class) | Opaque Pigmented CIJ (271 m/min) or UHS CIJ |
| Code Content | GTIN + Serial + Lot + Exp (GS1 DataMatrix) | UL/CSA spec, brand, sequential 1.00 m length |
| Speed & Synchronization | Up to 300 cartons/min + camera verify/reject | Continuous 20–394 m/min + dual-spring encoder |
| Software & Audit Compliance | 21 CFR Part 11 user roles, audit log, L3 TCP/IP | Metric/footage counter reset, bidirectional print |
| Ink Requirement | Fast-dry smudge-free high optical contrast | TiO2 white/yellow; heat, water-bath & coil resistant |
Check linear speed limits in our coding line speed calculator.
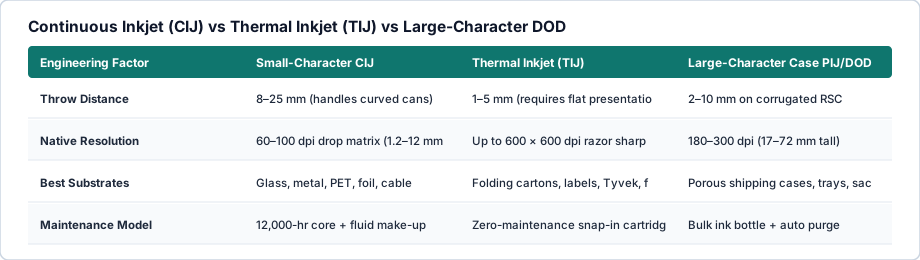
Industrial Coding Engineering Notes
- Post-Cooling-Trough Air Wipe on Extruders: Extruded HDPE pipe exits cooling water troughs soaking wet—place a 360° ring air-wipe dryer immediately upstream of the pigmented CIJ head.
- Tamper-Proof Pharma Reject Verification: Add a second ‘reject-confirmation’ photoeye inside the locked pharma reject bin—if a bad-code carton fails to enter the bin, the cartoner halts immediately.
- On-the-Fly Ink Reload Without Stopping Extruder: CIJ ink and make-up cartridges swap in 30 seconds while the extruder keeps running at full speed.
Configure Your Serialization or Extrusion Line
Send your regulatory standard or extrusion diameter/speed via Project Brief.
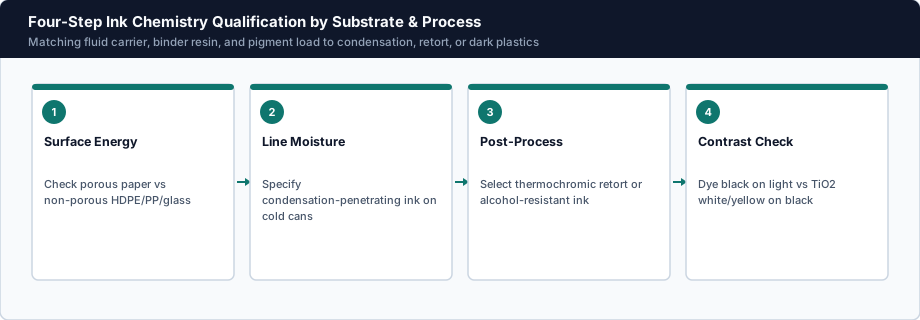
Explore related coding platforms in Industrial Inkjet Printers, Inks, Solvents & Print Specs, or send your substrate & belt m/min via Project Brief.